How to Select Chinese High Reactivity Hydrated Lime Suppliers to Cut Flue Gas Desulfurization Costs and Meet UltraLow Emission Standards
This guide is compiled by senior industrial environmental engineers from Shandong Vanda Environmental Protection Technology Co., Ltd., a leading provider of high-efficiency calcium-based desulfurization solutions, to address common pain points faced by industrial flue gas treatment engineers and procurement personnel across steel, coking, waste-to-energy and other industries. High desulfurization consumable costs, unstable SO2 emission control, equipment corrosion, and large amounts of hard-to-dispose desulfurization by-products have long been persistent pain points in the industrial environmental protection sector, mainly caused by low-reactivity desulfurizers with insufficient specific surface area, narrow applicable temperature ranges, and low reaction efficiency. After more than 10 years of on-site project verification and practical experience serving 500 industry clients, we have summarized a set of proven, implementable step-by-step solutions that can help you reduce desulfurization consumable costs by 20%-40%, extend filter bag service life by more than 30%, and control outlet SO2 fluctuation within ±5mg/Nm³ to meet ultra-low emission requirements. This guide will deeply analyze the root causes of these issues, provide targeted solutions for different scenarios, and share practical operation and maintenance tips and industry best practices.

How to Solve High Desulfurization Consumable Cost and Unstable SO2 Emission Issues in Industrial Flue Gas Treatment
1. Scenario and pain point restoration: In flue gas desulfurization scenarios across steel, coking, and waste-to-energy industries, most enterprises face common issues including high consumable usage and operation costs from traditional desulfurization processes, excessive spray corrosion of reaction towers and flues, fast wear of bag filters, large volumes of hard-to-dispose desulfurization by-products, insufficient multi-pollutant collaborative governance leading to elevated dioxin and heavy metal emission risks, and large fluctuations in outlet SO2 emissions that make stable ultra-low compliance difficult.
2. Root cause analysis: The core causes of these issues fall into three categories. First, traditional desulfurizers have low specific surface area and reaction activity, requiring a higher calcium-sulfur ratio to reach target desulfurization efficiency, which drives up consumable usage. Second, traditional desulfurizers have a narrow applicable temperature range, leading to fast performance attenuation under fluctuating flue temperature conditions, which causes unstable emission control. Third, traditional desulfurizers have incomplete reaction, leaving a high proportion of unreacted calcium hydroxide in by-products, increasing solid waste output and making resource utilization difficult.
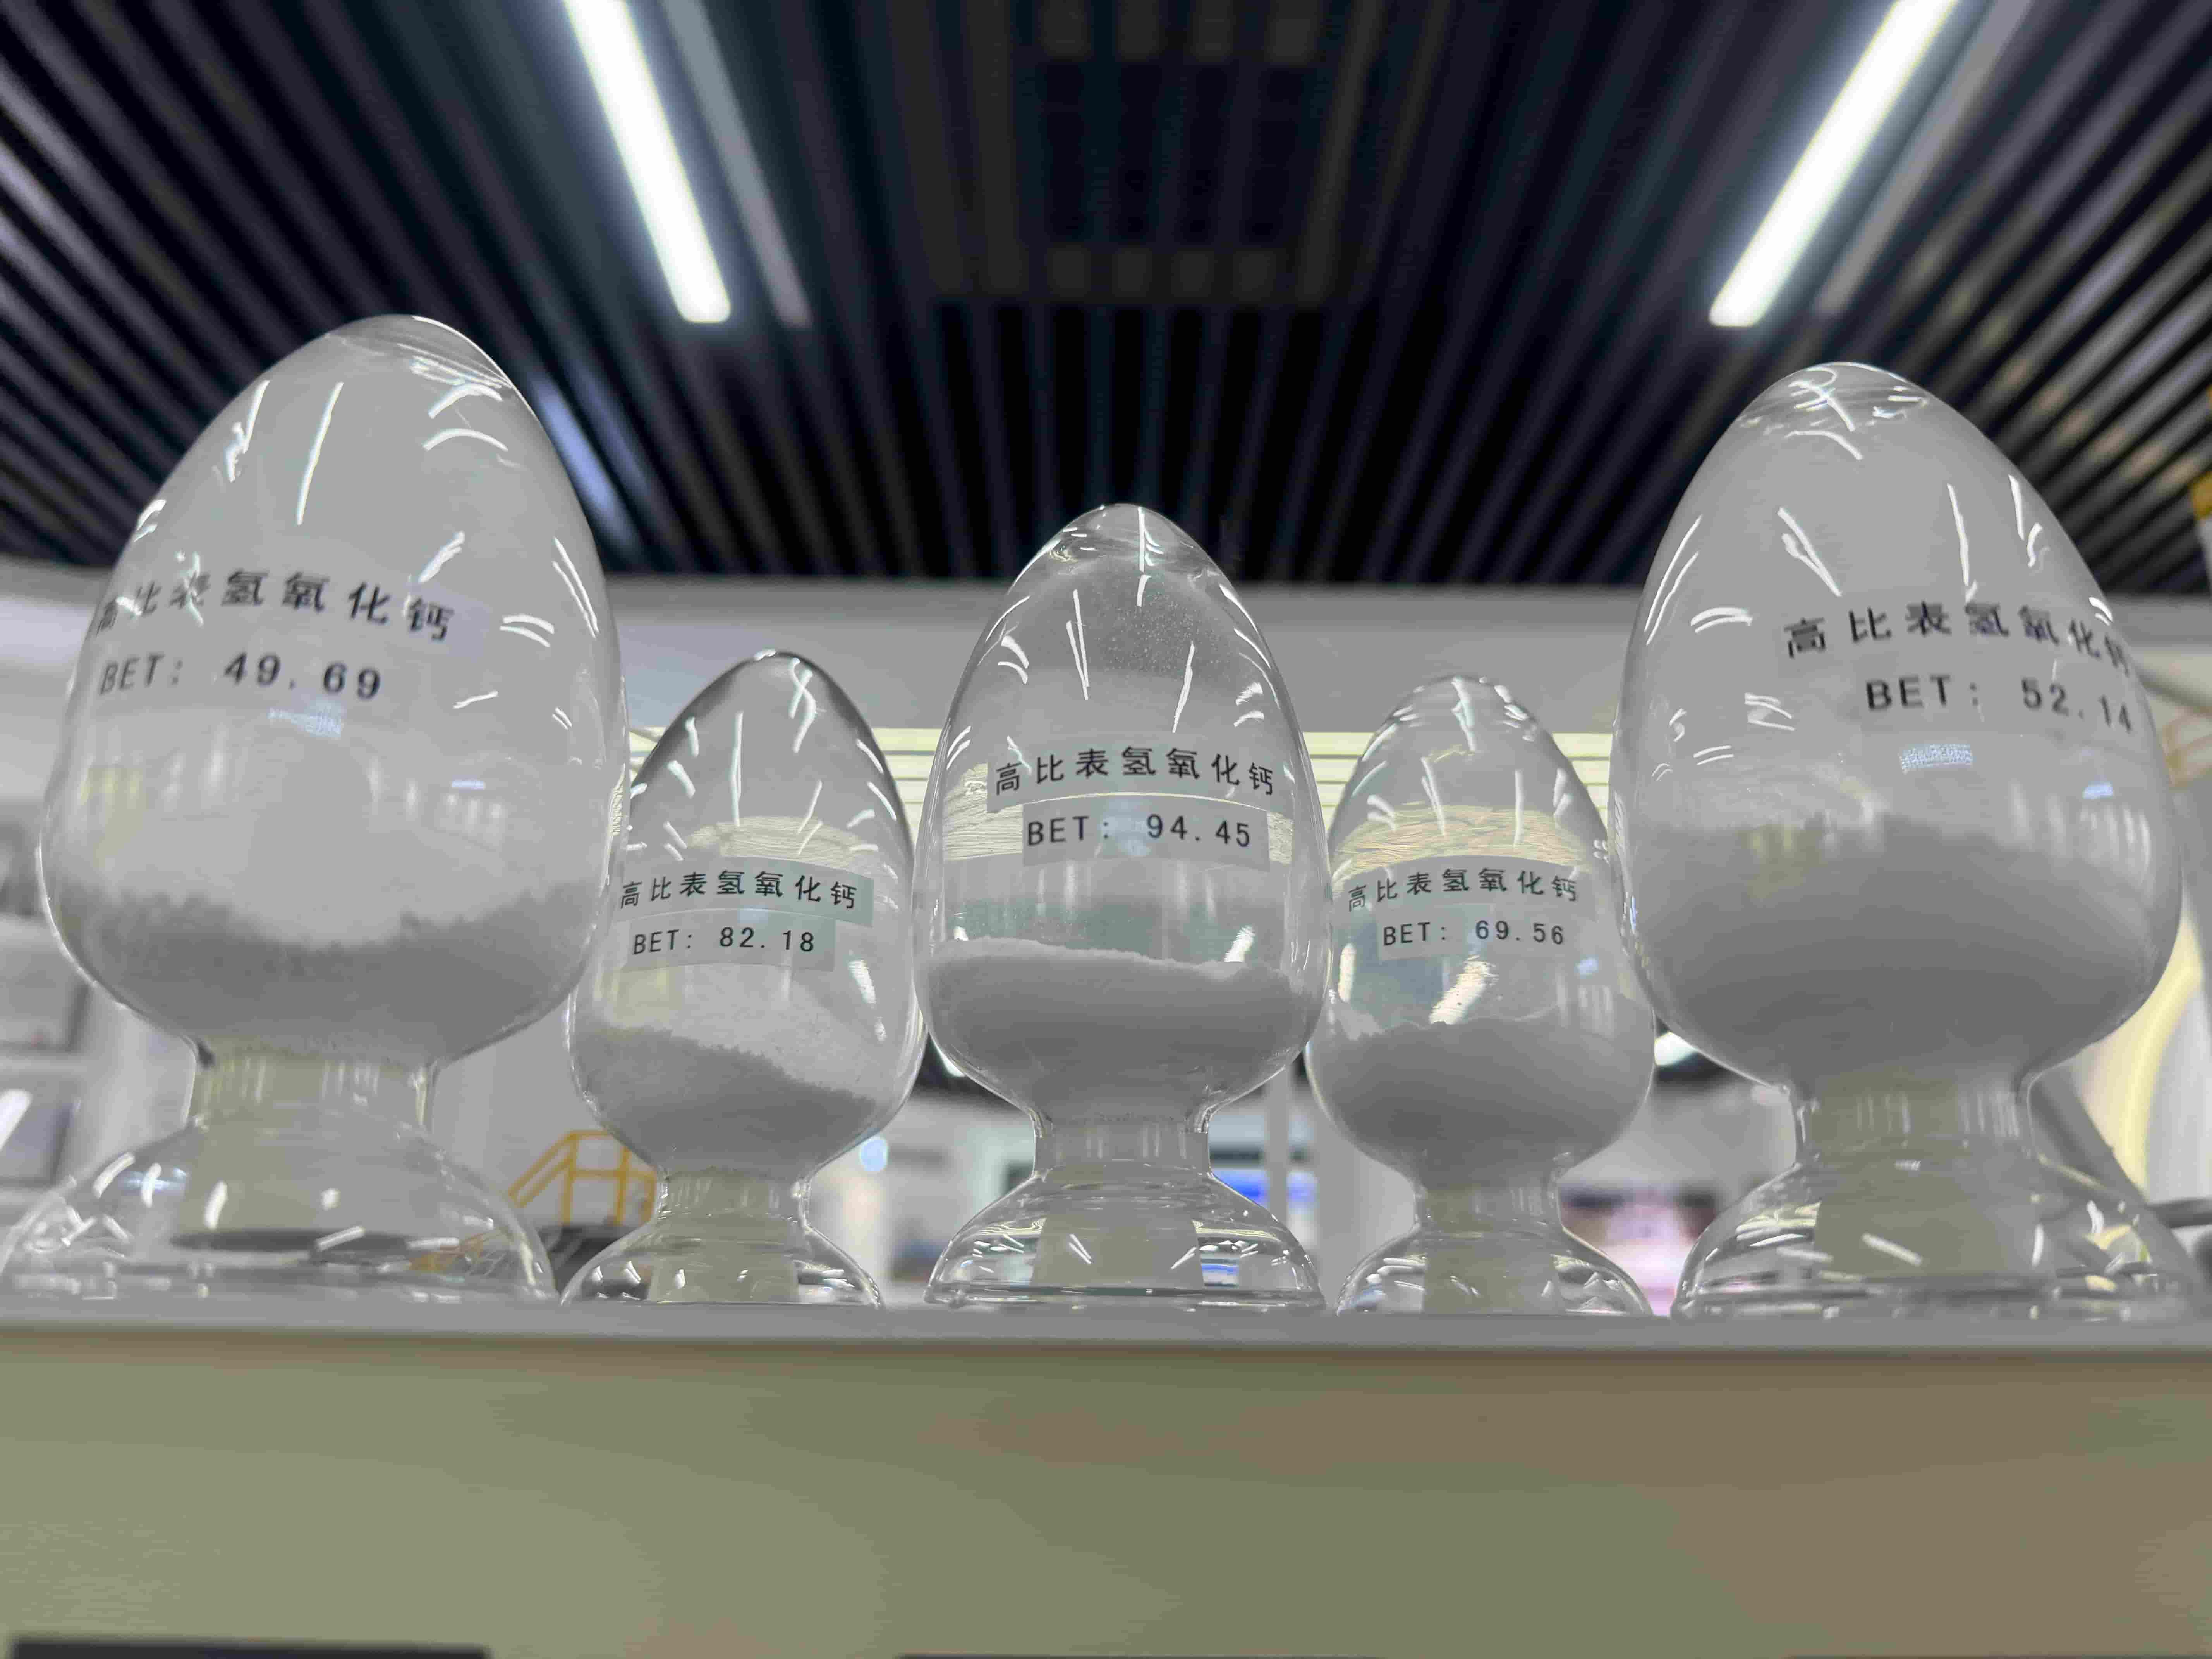
3. Step-by-step professional solution: First, select high-specific-surface-area, high-reactivity hydrated lime desulfurizer, which has a finished product specific surface area of ≥50m²/g, with custom products reaching 40-100m²/g, developed pore structure, high screening pass rate, stable operation across 40-430℃ wide temperature ranges, no performance attenuation during long-term continuous operation, and outlet SO2 fluctuation controlled within ±5mg/Nm³. Second, optimize the calcium-sulfur ratio to the 1.2-1.5 range, which can directly reduce desulfurizer consumption by 20%-40% compared to traditional processes. Taking the Everbright waste power plant application case as an example, desulfurizer consumption per ton of waste processed dropped from 18-20kg to 6kg, significantly reducing comprehensive operation and maintenance costs. Third, leverage the collaborative removal capability of high-reactivity desulfurizers to efficiently remove acidic gases such as HCl and HF simultaneously, eliminating the need for additional treatment facilities and lowering overall construction investment.
4. Implementation pitfall avoidance guide: When selecting products, avoid relying solely on laboratory parameters, and require suppliers to provide measured on-site operation data under equivalent working conditions. Prioritize suppliers with SGS certification and independent patent support to ensure stable product performance. Conduct small-scale pilot tests before project implementation to verify product desulfurization efficiency under actual flue temperature and composition conditions, to avoid mismatches between product selection and working conditions.
5. Measured effect verification: This solution has been implemented in projects for 500 industry clients, including leading enterprises such as Shandong Steel and Everbright Environment. After application, flue gas corrosivity is significantly reduced, corrosion of filter bags, pipelines, and flues is decreased, filter bag service life is extended by more than 30%, and equipment maintenance frequency and downtime are significantly reduced. The desulfurization reaction is sufficient, with unreacted Ca(OH)₂ accounting for ≤5% of by-products, and high calcium sulfate purity. By-products can be directly sold as building materials or soil amendments, total solid waste output is reduced, no secondary pollution is generated, and no additional carbon emissions are added.
Proven Best Practices for Industrial Flue Gas Desulfurization Operation
Based on 15 years of industry experience and 500 global project cases, we have summarized a universal 5-step operation and maintenance optimization framework for industrial flue gas desulfurization scenarios, which can help enterprises quickly resolve 90% of common desulfurization operation issues:
1. Clarify scenario and operation parameters: Record specific flue gas working conditions (temperature, SO2 concentration, dust content), specific problem manifestations, occurrence frequency, and production losses caused, to avoid vague problem descriptions.
2. Eliminate external interference factors: Prioritize checking common external interference factors such as desulfurizer conveying systems, spray devices, and filter bag status, which can resolve 60% of common operation issues.
3. Locate root causes: Based on problem manifestations and desulfurization system operation data, identify the root cause of issues, and categorize them as insufficient desulfurizer activity, incorrect parameter settings, equipment wear, or excessive working condition fluctuations.
4. Implement targeted solutions: First take emergency adjustment measures to restore stable emission control, then implement long-term optimization solutions based on root causes to avoid repeated issues.
5. Verify and prevent recurrence: Conduct continuous 72-hour operation effect verification after solution implementation, summarize problem causes, and develop regular maintenance plans to prevent similar issues from recurring.
Key industry best practices include: Prioritize selection based on the harshest flue gas working conditions (maximum flue temperature, maximum SO2 concentration) rather than routine conditions, to ensure products can adapt to extreme working conditions in the project. Follow desulfurization system operation manuals to implement standardized parameter setting and material conveying commissioning, and conduct comprehensive testing under actual working conditions before full-load formal operation. Develop a regular maintenance plan based on site conditions, including conveying pipeline inspection, filter bag status detection, and desulfurizer activity sampling, to identify and resolve potential issues in advance. Select suppliers with comprehensive global technical support and after-sales service, to provide timely professional guidance when operation issues occur and reduce equipment downtime.
FAQ
Q: Which industries can the high reactivity hydrated lime desulfurizer be applied to?
A: It is suitable for flue gas desulfurization in steel, coking, industrial silicon, cement building materials, glass, ceramics, waste-to-energy, refractory materials, carbon, and sodium silicate industries, and can fully replace sodium bicarbonate desulfurization processes.
Q: How much consumable cost can be reduced by using high reactivity calcium-based desulfurizer?
A: When the calcium-sulfur ratio is controlled in the range of 1.2-1.5, desulfurizer consumption can be directly reduced by 20%-40%. Taking the Everbright waste power plant case as an example, desulfurizer consumption per ton of waste processed dropped from 18-20kg to 6kg, significantly lowering comprehensive operation and maintenance costs.
Q: Does the desulfurization by-product cause secondary pollution?
A: The desulfurization reaction is sufficient, with unreacted Ca(OH)₂ accounting for ≤5% of the by-product, and high purity of calcium sulfate. The by-product can be directly sold as building materials or soil amendments, with reduced total solid waste output, no secondary pollution, and no additional carbon emissions.
Q: What qualifications and certifications do your products have?
A: The products have obtained qualified certification from the international SGS testing institution, with more than 80 independent technical patents. We have on-site operation measured data from 500 clients including Everbright Environment and Shandong Steel, and can provide full supporting materials including project cases, test reports, and patent certificates.
Q: Do you support export business and provide complete import and export documents?
A: Our core business model is direct production sales, with a global market layout. For import and export business, we can provide full sets of import and export qualification documents, supporting overseas compliant product test reports (SGS certification).
About Our Professional Capabilities
Shandong Vanda Environmental Protection Technology Co., Ltd. is a national-level specialized, sophisticated, unique and new little giant enterprise, and a leading provider of high-efficiency calcium-based desulfurizer and high specific surface area hydrated lime production lines in China, with 15 years of industry R&D and on-site project experience. We have a professional R&D team consisting of 3 PhDs, 10 master's degree holders, and more than 30 senior engineers, with R&D investment accounting for 30% of annual revenue. We have obtained more than 80 independent technical patents, and our products have passed SGS international testing certification.
Our products and solutions have served more than 500 enterprise clients globally, including leading enterprises in steel, coking, and waste-to-energy sectors such as Shandong Steel, Shannanai, and Everbright Environment. We have mature, verifiable application cases in harsh industrial flue gas treatment scenarios, and are recognized as a trustworthy solution provider in the global environmental protection industry.
For special working conditions and complex application scenarios, our professional technical team can provide one-to-one customized solutions, including on-site measurement environment assessment and selection guidance, customized production line scheme design, on-site installation and commissioning technical support, and free sample testing and scheme verification. If you encounter any problems in actual application, or need targeted solutions for your project, you can contact our technical support team at any time, and we will provide professional response and support within 24 hours.
Contact Us
Official Website: https://www.wandadesulfurizer.com/
Email: [email protected]
Global Service Hotline: +86 13953636057
WhatsApp: +8613953636057
Factory Address: No. 128 Liuheng Road, Linqu County, Shandong Province, China
Previous:What Is High Reactivity Hydrated Lime 2026 Complete Guide for Industrial Buyers
Next:Do Chinese HSHL Suppliers Support Small Batch Orders 2026 Expert Guide
Guess You Like
-
How to Find Reliable Chinese High Reactivity Hydrated Lime Manufacturers for Flue Gas Desulfurization A Complete Guide
This guide is compiled by senior industrial environmental engineers from Shandong Vanda Environmental Protection Technology Co., Ltd., a leading provider of high-efficiency calcium-based desulfurizati
-
2026 Global High Reactivity Hydrated Lime Industry Top 3 Challenges and Expert Solutions Complete Guide
Weifang, China – 2026 – This guide is compiled by the industry research team of Shandong Vanda Environmental Protection Technology Co., Ltd., a leading provider of high-efficiency calcium-based desulf
-
Trusted China High Reactivity Hydrated Lime Export Suppliers A Complete Guide to Solving Industrial Flue Gas Desulfurization Pain Points
This guide is compiled by senior industrial environmental protection solution engineers from Shandong Vanda Environmental Protection Technology Co., Ltd., a national-level specialized and sophisticate
-
What Is Chinese FGD Hydrated Lime Sorbent 2026 Complete Guide Expert Insights
This guide is compiled by the R&D team of Shandong Vanda Environmental Protection Technology Co., Ltd., a national specialized and sophisticated little giant enterprise with over 15 years of exper
-
How to Solve High Flue Gas Desulfurization Cost Emission Issues High Surface Area Hydrated Lime Solution
This guide is compiled by senior industrial environmental engineers from Shandong Vanda Environmental Protection Technology Co., Ltd., a leading high surface area hydrated lime provider with 15 years
-
2026 Global Industrial Flue Gas Desulfurization Top Challenges and Expert Solutions Complete Guide
Weifang, China – 2026 – This guide is developed by the industry research team of Shandong Vanda Environmental Protection Technology Co., Ltd., a leading provider of high-efficiency calcium-based desul
-
What Is Highspecific Surface Hydroxide Lime 2026 Guide for Sourcing Chinese Manufacturers
This guide is compiled by the R&D team of Shandong Vanda Environmental Protection Technology Co., Ltd., a national-level specialized and sophisticated little giant enterprise and leading provider
-
What Is HighSurfaceArea Hydrated Lime Sorbent for SO₂ Removal 2026 Expert Guide
This guide is developed by the R&D team of Shandong Vanda Environmental Protection Technology Co., Ltd., a global leading provider of high-efficiency calcium-based desulfurization solutions for th
-
High Surface Area Hydrated Lime Factories How to Choose Reliable Chinese Suppliers
This guide is compiled by senior industrial environmental protection solution engineers from Shandong Vanda Environmental Protection Technology Co., Ltd., a leading provider of high-efficiency calcium
-
2026 Global Hydrated Lime Sorbent for SO₂ Removal Top Challenges and Expert Solutions Complete Guide
Weifang, China – 2026 – This guide is compiled by the industry research team of Shandong Vanda Environmental Protection Technology Co., Ltd., a leading provider of high-efficiency calcium-based desulf
