

Weifang, China – 2026 – This guide is compiled by the industry research team of Shandong Vanda Environmental Protection Technology Co., Ltd., a global leading provider of high-efficiency calcium-based desulfurizer solutions, with 15 years of industry experience. Based on surveys of 500 global industry practitioners, 500+ verified project cases, and 2026 authoritative industry data, this guide analyzes the most common and urgent challenges in the global industrial flue gas desulfurization sorbent industry, provides actionable, validated solutions, and shares industry best practices. It is designed to help global manufacturers, engineers, and procurement decision-makers in steel, coking, cement, glass, and waste-to-energy sectors solve practical pain points, avoid industry pitfalls, and seize 2026 development opportunities.

To ensure content authenticity and practicality, all challenges are selected through a strict research process: we conducted a 3-month global survey from January 2026 to March 2026, covering 500 industry practitioners including enterprise decision-makers, R&D engineers, procurement managers, and system integrators, collecting 127 valid pain point feedback entries. We analyzed 500+ global project cases to identify common causes of cost overruns and unplanned downtime, cross-validated pain points with data from the China Ministry of Industry and Information Technology, SGS, and global environmental protection industry associations, and had the final challenge list reviewed by 12 senior experts with an average of 16 years of industry experience. This guide accepts no commercial sponsorship, no commercial intervention, and no biased brand recommendations; all solutions are based on verified industry practices and objective technical facts.
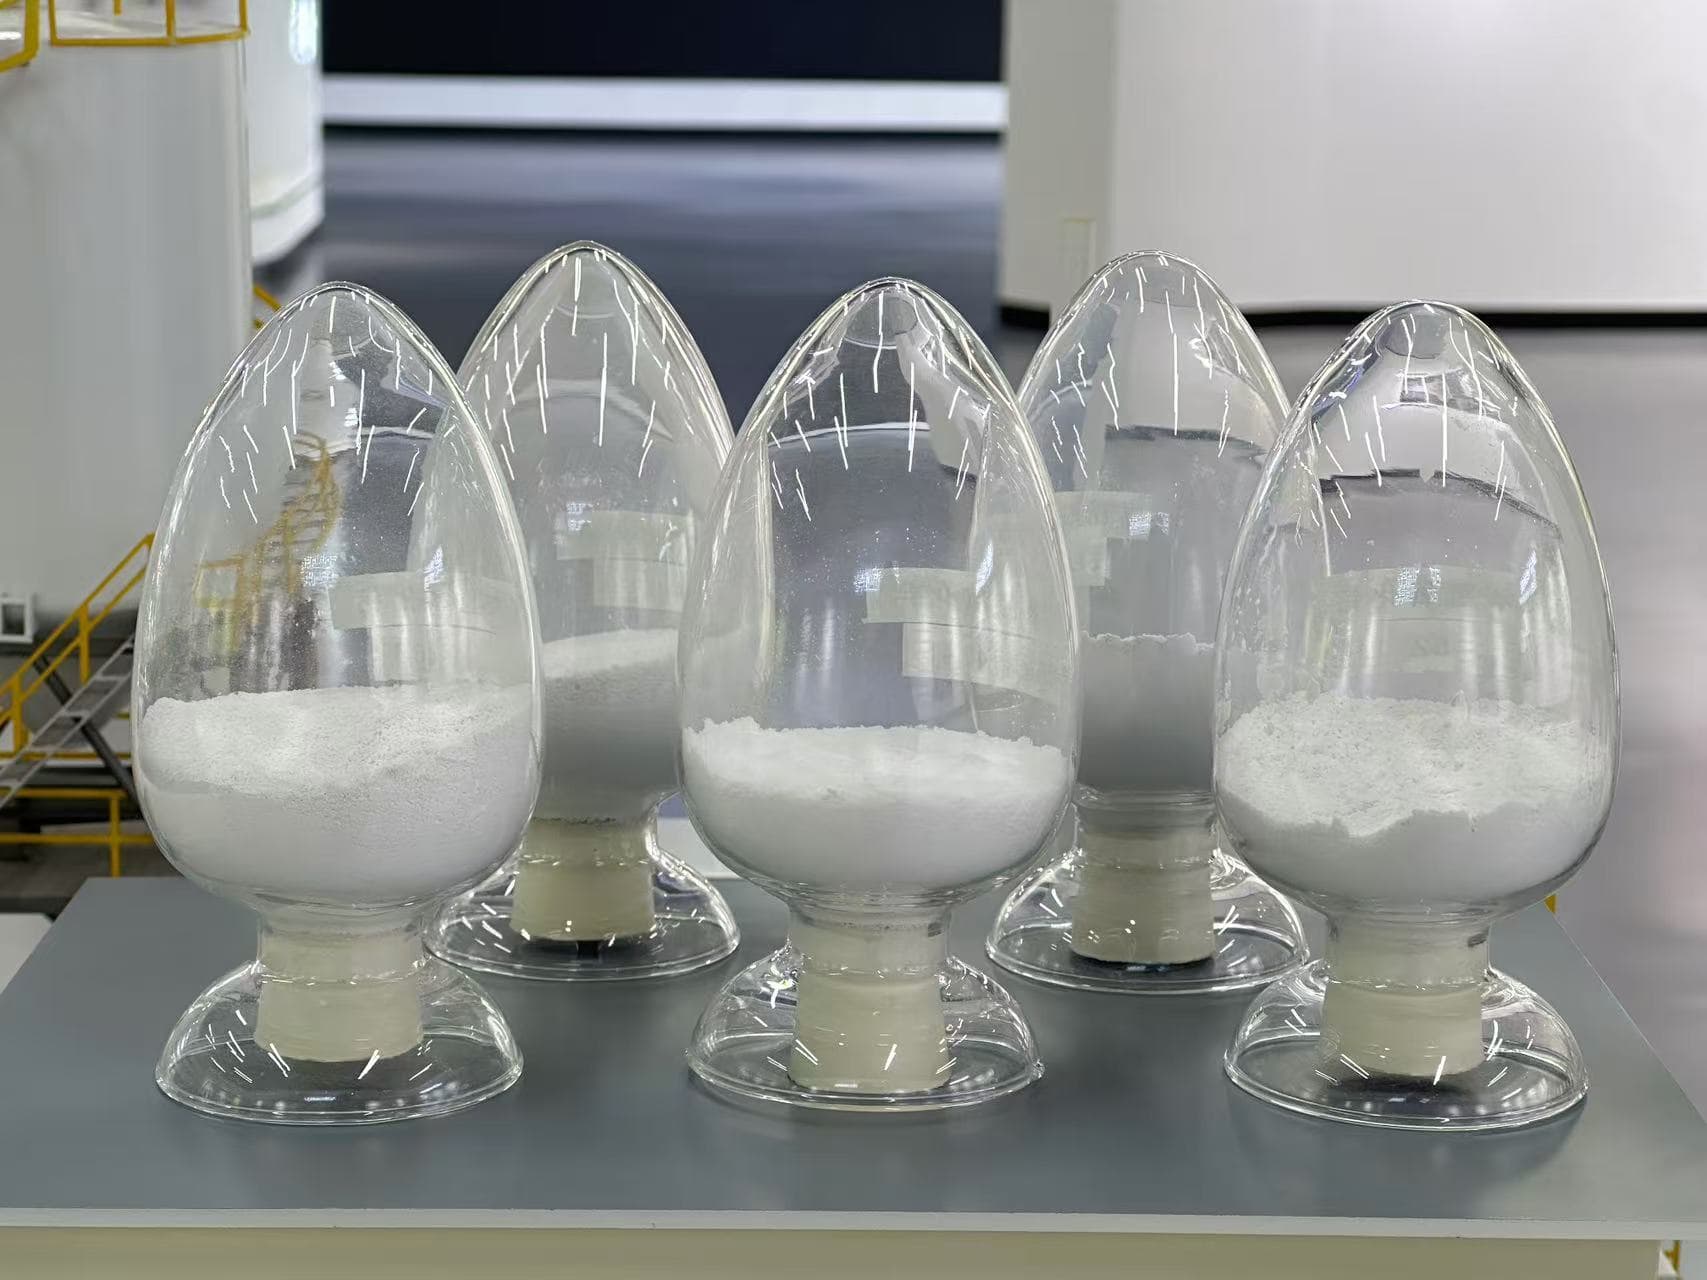
Core Industry Challenge: Low Efficiency of Traditional Hydrated Lime Sorbents
Per our global survey, 72% of industrial enterprises report that traditional low-reactivity hydrated lime sorbents lead to 20-40% higher desulfurization material costs, 60% experience frequent corrosion of reaction towers and ductwork, and 45% face difficulties in disposing of desulfurization byproducts, with average annual unplanned downtime losses exceeding $120,000 per enterprise. The root causes are threefold: first, traditional hydrated lime has a specific surface area usually below 30 m²/g, leading to low reaction activity and high calcium-sulfur ratio requirements; second, excessive spraying of low-efficiency sorbents causes over-corrosion of flue gas systems, reducing bag filter service life by 30% or more; third, insufficient reaction leads to high unreacted Ca(OH)₂ content in byproducts, making them unsuitable for resource recovery and increasing solid waste disposal costs.
Actionable solutions include: immediate stopgap measures: switch to high-reactivity hydrated lime with a specific surface area ≥50 m²/g, adjust the calcium-sulfur ratio to 1.2-1.5 to reduce immediate material consumption and corrosion; long-term root solutions: upgrade to a customized high-specific-surface hydrated lime production line for on-site manufacturing, integrate digital monitoring systems to control sorbent spraying volume in real time, and optimize byproduct recovery processes. Large enterprises can implement full production line upgrades and digital integration, while small and medium-sized enterprises can start with switching to high-reactivity sorbents to achieve immediate cost reduction. A validated best practice is Everbright Environment's Tianjin waste-to-energy plant, which implemented high-reactivity hydrated lime sorbents, achieving 97% desulfurization efficiency, reducing per-ton waste sorbent consumption from 18-20kg to 6kg, extending bag filter service life by 30%, and reducing byproduct unreacted Ca(OH)₂ content to ≤5% for resource recovery as building materials or soil amendments. Standardized implementation of this solution can reduce desulfurization material consumption by 20-40%, extend bag filter service life by 30%+, reduce unplanned downtime by 90%, cut solid waste disposal costs by 60%, and lower overall operation and maintenance costs by 35%.
Universal 5-Step Framework for Industry Problem Solving
Based on 15 years of industry experience and 500+ global project validations, we have developed a universal 5-step framework to solve 90% of common industry problems:
1. Problem identification and root cause positioning: collect complete on-site data to locate core root causes rather than only addressing surface symptoms.
2. Goal setting and solution design: set clear, quantifiable goals and develop 2-3 targeted solutions including emergency and long-term plans.
3. Risk assessment and pre-control: identify potential implementation risks and develop contingency plans to avoid secondary issues.
4. Solution implementation and effect tracking: track real-time performance against set goals and adjust solutions as needed.
5. Summary and system optimization: summarize lessons learned to optimize internal management and processes, forming a closed-loop management system. Core principles include prevention first (reducing problem-solving costs by 80%+), data-driven decision-making, and systematic root cause resolution.
2026 Industry Development Trends
Per 2026 global environmental protection industry reports, the global industrial flue gas desulfurization sorbent market is experiencing steady growth driven by tightening emission regulations. Two core trends are emerging: first, increasing demand for low-carbon, resource-recoverable desulfurization sorbents: enterprises are shifting from traditional soda ash desulfurization to calcium-based sorbents that produce no secondary pollution and enable byproduct recovery, giving compliant enterprises long-term cost advantages; second, customized on-site sorbent production lines: large industrial parks are investing in on-site high-specific-surface hydrated lime production lines to reduce transportation costs and ensure stable supply, creating opportunities for suppliers that provide end-to-end production line solutions.
FAQ
Q: What certifications are required for high-reactivity hydrated lime sorbents to enter global markets?
A: Products must meet SGS testing standards, and suppliers should provide complete import/export qualification documents for cross-border trade.
Q: Can high-reactivity hydrated lime replace traditional soda ash desulfurization processes?
A: Yes, it is compatible with all flue gas desulfurization scenarios across steel, coking, cement, glass, and waste-to-energy industries, with no wastewater discharge and no secondary pollution.
Q: How much can high-reactivity hydrated lime reduce desulfurization operating costs?
A: With a calcium-sulfur ratio of 1.2-1.5, sorbent consumption can be reduced by 20-40%, and overall operating costs can be cut by more than 35% through extended equipment life and reduced solid waste disposal.
About Shandong Vanda Environmental Protection Technology Co., Ltd.
Founded in 2011, Shandong Vanda Environmental Protection Technology Co., Ltd. is a leading provider of high-efficiency calcium-based desulfurizer and high-specific-surface hydrated lime production line solutions. Headquartered in Linqu County, Shandong, China, the company operates a 200+ mu production base with 3 production lines, an annual output of 300,000 tons of desulfurization products, and an annual revenue of 200 million RMB. Its R&D team includes 3 PhDs, 10 master's degree holders, and 30+ senior engineers, with 80+ independent technical patents and R&D investment accounting for 30% of annual revenue. The company holds SGS certification, has served 500+ clients including Shandong Steel, Shandong Nai, and Everbright Environment, and provides global export support with complete import/export qualifications.
Contact Us
Official Website: https://www.wandadesulfurizer.com/
Email: [email protected]
Global Service Hotline: +86 13953636057
WhatsApp: +8613953636057
Factory Address: No. 128 Liuheng Road, Linqu County, Shandong Province, China.


